

Washed PP/PE film regrind is one of the most valuable — and most difficult — feedstocks in plastic recycling. After washing, film flakes still carry residual moisture, printing inks, and low-molecular-weight volatiles that a basic pelletizer cannot handle. The result is often dark, smelly pellets with poor melt strength that buyers reject. The two-stage PP/PE film pelletizing line described here is engineered specifically for this challenge: it takes film regrind straight from the washing plant and converts it into clean, dry, uniform pellets ready for film blowing, pipe extrusion, or injection molding.
洗浄済みフィルム粉砕物に専用ペレット化ラインが必要な理由
Not all pelletizing lines are equal when the feedstock is washed film. Compared with rigid regrind, film flake has a very low bulk density, wraps easily around screws, and traps water in its folds even after mechanical drying. Printed films — shopping bags, packaging films, agricultural mulch film — add another layer of difficulty: ink residues and paper labels break down into volatiles during melting, causing odor, discoloration, and bubbles in the final pellet.
A conventional single-stage extruder forces all of these problems through one short process: melt, filter once, pelletize. Moisture flashes into steam inside the barrel, ink volatiles have nowhere to escape, and the single filter clogs quickly. Throughput drops, pellet quality suffers, and operators spend more time changing screens than running the line. This is why recyclers processing washed film increasingly specify a two-stage system with vacuum degassing and segmented filtration — the configuration this プラスチックリサイクル用ペレタイジングマシン line is built around.
作動原理
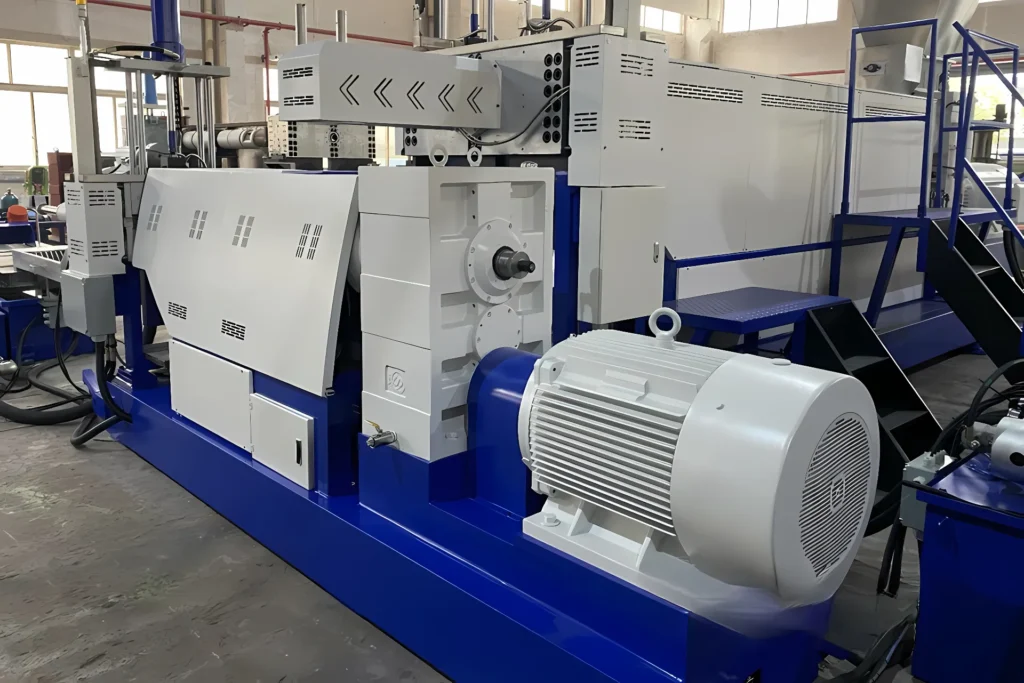
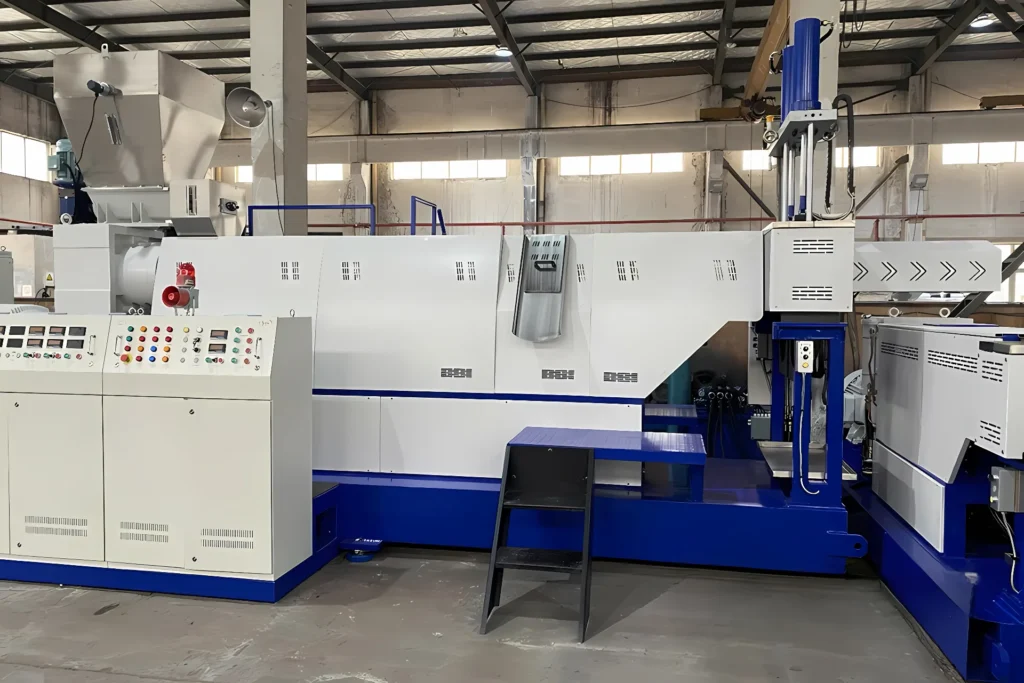
The line processes film regrind in four continuous stages. Each stage addresses a specific weakness of washed film feedstock:
- 供給。 The film regrind is fed into the dosing feeder through a screw conveyor. When the electric current of the extruder exceeds the preset level, the dosing feeder and feeding screw conveyor halt automatically. This current-based interlock prevents overfeeding — the most common cause of surging and degraded melt in film extrusion — and keeps the process stable even when flake bulk density varies from batch to batch.
- 可塑化と脱ガス。 A customized single screw extruder gently melts the film regrind. The plastic scraps are thoroughly melted and plasticized in the first-stage extruder, then conveyed into the second-stage extruder for further homogenization. Between the stages, a double-zone vacuum degassing system pulls out volatiles such as low-molecular-weight compounds and residual moisture. This step is what makes the system particularly suitable for heavily printed films and material with some moisture content: ink gases and steam are extracted before they can become trapped in the melt.
- 溶融濾過。 The line follows a segmented filtering principle: pre-filtering is completed in the first extruder, while fine filtering is done in the second extruder. Coarse contaminants — paper fibers, aluminum flecks, unmelted gels — are caught early so they never reach the fine screen. Because the filtration load is split across two stages, the frequency of replacing filter sieves drops significantly, which means longer continuous runs and lower consumable costs.
- ペレット化。 The homogenized, degassed, and twice-filtered melt is cut by a die-face water-ring pelletizing system. To deliver optimally dried pellets, the cutter is paired with an advanced dewatering vibration sieve followed by horizontal-type centrifugal dewatering. Pellets leave the line with low surface moisture, ready for bagging or direct feeding into downstream production.
フィルム粉砕物には二段押出が一段押出より優れている理由
The difference between one extruder and two is not just capacity — it is process separation. In a single-stage machine, melting, degassing, and fine filtration must all happen in one barrel, which forces compromises: raise the temperature for better melting and you risk degrading heat-sensitive material; open the vent wider for degassing and you lose melt pressure needed for fine filtration.
A two-stage line decouples these functions. The first extruder focuses on gentle, complete plasticization and coarse filtration. The second extruder receives an already-homogeneous melt, so it can run the vacuum degassing and fine filtration under ideal conditions. The practical payoff for washed film recyclers:
- Better pellet color and odor — volatiles from inks and labels are removed under vacuum instead of being sealed into the pellet.
- Higher melt quality — two plasticization passes break down gels and unmelted particles more completely than one.
- Fewer screen changes — segmented filtration spreads the contaminant load, extending screen life.
- More stable throughput — the current-interlocked dosing feeder keeps the first stage from overfeeding, so output stays consistent across varying flake quality.
For comparison, a twin-screw extruder pelletizing solution excels at compounding and heavily filled materials, while this two-stage single-screw configuration is optimized for the specific pain points of washed film: moisture, ink, and low bulk density.
主な特長
- Two-stage single-screw extrusion — two extruders in series for superior melt homogeneity and pellet quality versus single-stage designs.
- Double-zone vacuum degassing — removes moisture, ink volatiles, and low-molecular-weight compounds; handles printed films and damp regrind that choke ordinary pelletizers.
- Segmented filtration — pre-filter on the first stage, fine filter on the second; fewer sieve changes and longer uninterrupted runs.
- Current-interlocked auto feeding — the dosing feeder and screw conveyor stop automatically when extruder current exceeds the preset, protecting the screws and stabilizing output.
- Die-face water-ring cutting — uniform pellet size with clean cut faces, better for downstream feeding than strand pelletizing on film grades.
- Two-step dewatering — vibration sieve plus horizontal centrifugal dewatering for low-moisture pellets straight off the line.
PP/PEフィルムペレット化の用途
Pellets produced by this line are clean, dry, and consistent enough to feed directly back into production. Typical downstream uses include:
- Film blowing — recycled pellets blended with virgin resin for shopping bags, garbage bags, and agricultural film.
- Pipe extrusion — PE pellets for drainage pipe, corrugated pipe, and cable conduit where color consistency matters less than melt strength.
- Injection molding — PP pellets for crates, pallets, flower pots, and other thick-walled parts.
- Woven bag and raffia production — when paired with the right filtration fineness, pellets suit tape extrusion lines; see our PP/PE film and woven bag water-ring pelletizing system for a dedicated configuration.
If your feedstock is PET flake rather than film, a single-screw pelletizer for PET flakes is the more appropriate choice — film lines and PET lines differ fundamentally in drying and IV requirements.
技術仕様
Four models cover 200 to 1,000 kg/h. Select based on your washing line output — the pelletizing line should match or slightly exceed the washer’s hourly flake production to avoid becoming the bottleneck.
| 機械サイズ | 効率容積(リットル) | モーター出力(KW) | スクリュー直径(mm) | L/D | 押出機モーター出力(KW) | 処理能力(kg/h) |
|---|---|---|---|---|---|---|
| PE-250 | 300 | 1.1 | 120/130 | 30/10 | 110-132 | 200-300 |
| PE-500 | 500 | 2.2 | 140/150 | 30/10 | 132-160 | 400-500 |
| PE-800 | 800 | 3.0 | 160/180 | 30/10 | 220-250 | 700-800 |
| PE-1000 | 1000 | 4.0 | 180/200 | 30/10 | 280-315 | 800-1000 |
追加画像



適切なフィルムペレット化ラインの選び方
Before requesting a quote, confirm these points so the line is sized and configured for your actual feedstock:
- Washer output — what is your washing line’s hourly flake output? Size the pelletizer to match or slightly exceed it.
- Print coverage — what share of the film is printed? Heavy print loads make vacuum degassing essential, not optional.
- Moisture after drying — what is the flake moisture content leaving your dryer? Above ~5% and you will want the full dewatering package.
- 汚染レベル — paper labels, aluminum, sand? This determines the filtration fineness and screen-change interval to expect.
- Target pellet application — film blowing needs the finest filtration and best degassing; pipe and injection tolerate more.
- Power and space — confirm voltage, compressed air, cooling water supply, and floor space for the full line including dewatering.
For background on upstream film handling, see our プラスチックフィルム絞り機ガイド そして本文は PP/PEフィルムペレット化機 overview.
よくあるご質問 (FAQ)
一段フィルムペレット化と二段フィルムペレット化の違いは何ですか?
A single-stage extruder melts, degasses, and filters in one barrel, forcing compromises on temperature and pressure. A two-stage line separates plasticization and coarse filtration (first extruder) from vacuum degassing and fine filtration (second extruder), producing cleaner, drier pellets with fewer screen changes — especially important for printed or damp washed film.
このラインは印刷済みフィルムや水分を含む原料に対応できますか?
Yes. The double-zone vacuum degassing system is designed to extract ink volatiles, low-molecular-weight compounds, and residual moisture between the two extrusion stages. This makes the line suitable for heavily printed films and regrind with some moisture content that would cause odor and bubbles in a basic pelletizer.
このラインはどのペレット化方式を採用していますか?
Die-face water-ring pelletizing. The melt is cut directly at the die face into a water ring, which gives uniform pellet size and clean cut faces. The pellets then pass through a dewatering vibration sieve and horizontal centrifugal dewatering for low surface moisture.
どの程度の処理能力が得られますか?
Four models cover 200 to 1,000 kg/h: PE-250 (200–300 kg/h), PE-500 (400–500 kg/h), PE-800 (700–800 kg/h), and PE-1000 (800–1,000 kg/h). Actual output depends on film type, contamination level, and filtration fineness. Size the line to match or slightly exceed your washing line’s flake output.
再生ペレットはどのような用途に使用できますか?
The pellets can feed directly into film blowing (shopping bags, garbage bags, agricultural film), pipe extrusion (drainage and corrugated pipe), and injection molding (crates, pallets, thick-walled parts). For woven bag and raffia tape extrusion, confirm the filtration fineness with the supplier.
フィルタースクリーンはどのくらいの頻度で交換が必要ですか?
Less often than on a single-stage line. The segmented filtering principle — pre-filtering in the first extruder, fine filtering in the second — splits the contaminant load across two screens, extending change intervals. Exact frequency depends on contamination level; paper and aluminum content are the main drivers.
このラインには乾燥機能が含まれていますか、それとも別途乾燥機が必要ですか?
The line includes vacuum degassing (which removes internal moisture during extrusion) plus two-step surface dewatering after cutting. It is designed to take flake from a washing plant with normal residual moisture. If your flake arrives soaking wet, add mechanical pre-drying upstream for best results.
ペレット化ラインを見て見積もりを依頼する
Tell us your washing line output, film types, and target pellet application, and we will recommend the right model and configuration. See the プラスチックペレタイザー機 range and request a quote.
